CN
Company Profile

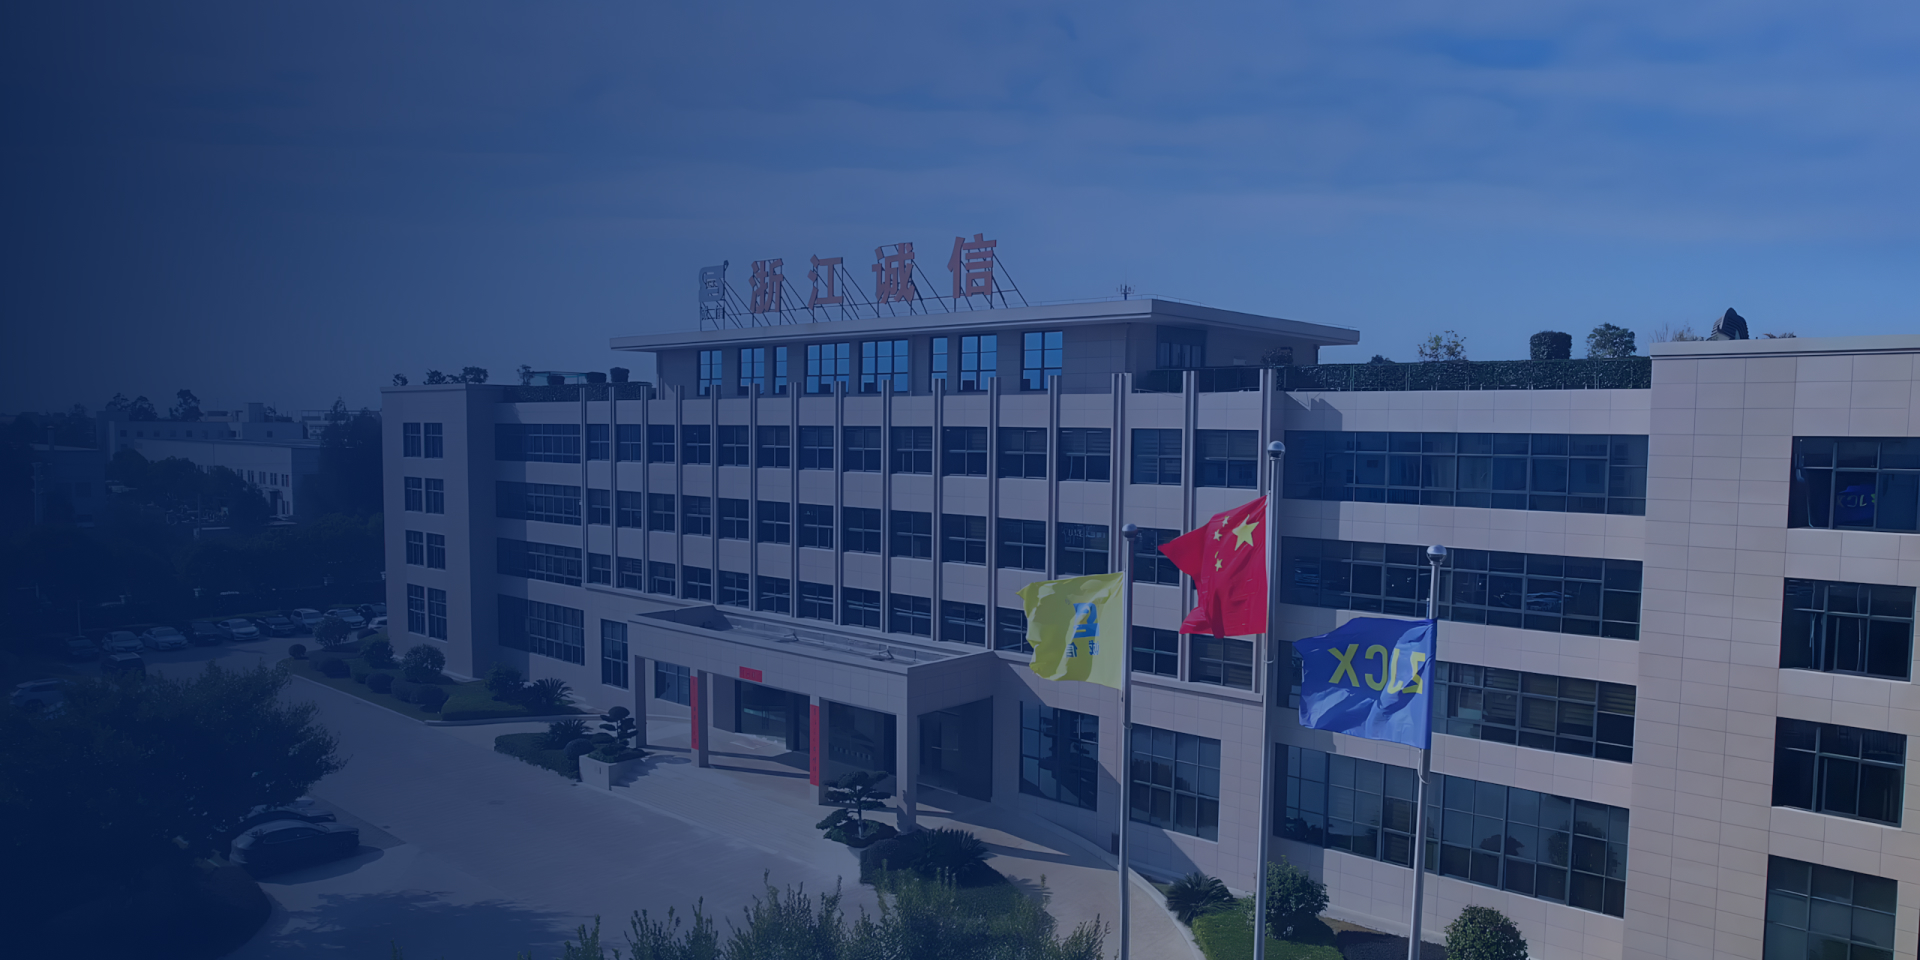
Zhejiang Chengxin Medical and Chemical Equipment Co., Ltd. is a company certified for the design of stationary pressure vessels and the manufacture of Class A2 pressure vessels. It holds the ASME “U” stamp from the American Society of Mechanical Engineers, CNAS laboratory accreditation, and GC2 pipeline installation certification, among other qualifications. The company focuses on providing advanced, eco-friendly, safe, and reliable equipment for modern pharmaceutical, chemical, and petrochemical enterprises, offering customers high-quality process equipment system solutions. Founded in 1992 with a registered capital of 81.68 million yuan, the company has kept pace with the times and continued to move forward since its inception. After more than 30 years of development, it has grown into an industry leader. The company currently employs over 750 staff members, including more than 180 senior and intermediate technical personnel, 5 senior engineers, 3 provincial-level master craftsmen, 2 senior technicians, 12 intermediate technicians, and 20 technical advisors (comprising authoritative experts and professors specially appointed by the company).

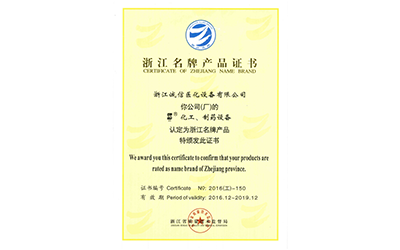
The company is a national-level “Specialized, Refined, Unique, and Innovative” (“Little Giant”) enterprise; a member of the China Pharmaceutical Equipment Association and the China Chemical Equipment Association; a nationally certified high-tech enterprise; a Zhejiang Provincial Green and Low-Carbon Factory; a recipient of the Zhejiang Provincial “First-of-its-Kind” Equipment Award; a Zhejiang Provincial Credit Management Model Enterprise; a Zhejiang Provincial Intellectual Property Model Enterprise; a Zhejiang Provincial Water-Conserving Enterprise; a Taizhou City “Gazelle” Enterprise; a district-level Meritorious Enterprise; and a recipient of the District Government Quality Award. The company has obtained certifications for the ISO 9001 Quality Management System, ISO 14001:2015 Environmental Management System, ISO 45001:2018 Occupational Health and Safety Management System, ISO 50001:2018 Energy Management System, Information Technology and Industrialization Integration Management System, Intellectual Property Management System, and centrifuge mechanical safety, among others. In 2016, the “Integrity” brand chemical and pharmaceutical equipment was recognized as a Zhejiang Famous Brand Product. Currently, the company holds more than 120 intellectual property rights, including over 40 invention patents.

The company has established a provincial-level enterprise technology center, a provincial-level enterprise research institute, and a provincial-level postdoctoral workstation. It has successively collaborated on scientific and technological projects with research institutions and leading universities such as the Chinese Academy of Sciences, Zhejiang University, Zhejiang University of Technology, Tongji University, and Beijing University of Chemical Technology. The company has been approved as the national-level “Ministry of Education Engineering Research Center for Process Equipment and Its Remanufacturing,” serves as a joint training base for professional degree graduate students in mechanical engineering at Zhejiang University of Technology, and has co-established the “Green Process Equipment R&D Center” with Zhejiang University.

The company strictly adheres to GMP certification standards and possesses the capability to manufacture extra-large equipment to meet customers’ special requirements. Its market network spans both domestic and international markets, serving over 500 clients, with offices established in Jiangsu, Jiangxi, Hunan, Shanghai, Guangdong, Chongqing, Hebei, and other regions.

The company consistently upholds the corporate spirit of “Integrity, Dedication, Excellence, and Innovation,” adheres to the spirit of craftsmanship, and is committed to contributing integrity and expertise to the transformation and upgrading of the pharmaceutical and chemical industries through exceptional products and services!
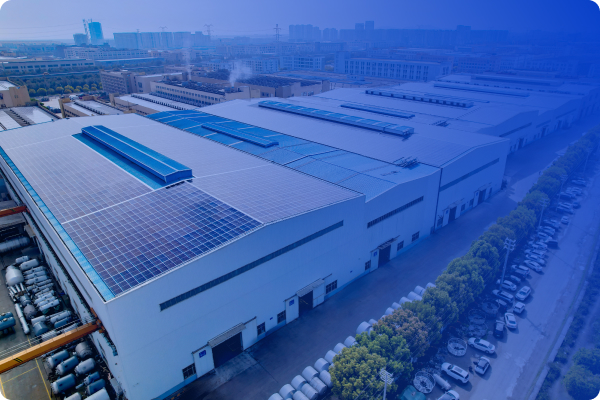
Over 30 Years of Experience
Crafting Excellence with Dedication

Guided by its core values of integrity, dedication, excellence, and innovation, the company remains committed to fine craftsmanship and leverages Chengxin’s expertise and ingenuity to support the transformation and advancement of the pharmaceutical and chemical industries.

Chengxin Pharm & Chem Equipment holds comprehensive management system certifications, and its products have received the Zhejiang Famous Brand designation. Serving more than 700 customers in China and overseas, the company is a leader in the pharmaceutical and chemical equipment industry.

Founded in 1992, Zhejiang Chengxin Pharma& Chem Equipment Co., Ltd. is a nationally recognized specialized and innovative “Little Giant” enterprise and a National High-Tech Enterprise. It holds a Class A2 pressure vessel manufacturing license, authorization to use the ASME Certification Mark with the “U” Designator, CNAS laboratory accreditation, and a GC2 industrial piping installation license. The company specializes in providing green, safe, intelligent, and reliable process equipment and integrated system solutions for the pharmaceutical, chemical, semiconductor, and advanced materials industries.

Million RMB

Registered Capital

Full-Time Employees

Mid-and Senior-Level Technical Professionals

Proprietary Intellectual Property Rights

Customers in China and Overseas

To become a developer and manufacturer of cutting-edge equipment for modern process industries

Crafting excellence with dedication, leading the industry through innovation, and creating lasting value for high-quality industrial development and the green transition

Corporate Vision
Development Strategy

Keeping Pace with the Times and Moving Forward

Technological Innovation Strategy

Focus on the R&D of high-end equipment, strengthen collaboration among industry, academia, and research institutions, achieve breakthroughs in key core technologies, and enhance the ability to commercialize invention patents and first-of-a-kind products.

Quality Leadership Strategy

Ensure strict compliance with GMP requirements and international standards, pursue excellence in product quality, and strengthen our position as an industry benchmark and market leader.

Digital Empowerment Strategy

Powered by AI and connected through data, we integrate the full value chain across R&D, production, supply chain, and services. Through digitalization and intelligent technologies, we improve management efficiency, drive business innovation, and transform our operating model.

Global Market Expansion Strategy

Optimize our domestic network, expand into overseas markets, and build a global sales and service network.

Talent-Driven Development Strategy

Recruit and develop high-caliber technical professionals and skilled personnel to strengthen our core competitiveness across the entire R&D, manufacturing, and service value chain.

Development Milestones

Working together to create a better future

1992

● In June, Dongshan Chemical Machinery Factory was established

1998

● In October, the company obtained ISO 9001 quality management system certification

2005

● In January, the company was renamed Zhejiang Chengxin Pharm & Chem Equipment Co., Ltd.

● In September, it became a member of the China Association for Pharmaceutical Equipment

● In December, it obtained Class D1 and D2 manufacturing licenses for Category I and II pressure vessels

2008

● In August, the company expanded Chengxin Plant II

● In November, its inverting filter centrifuge project was approved for support under the National Innovation Fund

● In December, the centrifuge obtained mechanical safety certification

2009

● In August, the company jointly established the Pharmaceutical and Chemical Equipment Engineering Technology R&D Center with Zhejiang University of Technology

● In November, it collaborated with the Chengdu Institute of Organic Chemistry, Chinese Academy of Sciences, on a pervaporation membrane technology development project

● In December, it obtained a Class A2 manufacturing license for Category III pressure vessels

2010

● In October, the “Chengxin” trademark was recognized as a Famous Trademark of Taizhou

● In November, the company was recognized as a National High-Tech Enterprise

● In December, the CSMB project received Second Prize in the Ministry of Education’s Technological Invention Awards

2011

● In April, the company obtained ISO 14001 environmental management system certification and OHSAS 18001 occupational health and safety management system certification

● In October, it was named one of Zhejiang Province’s 100 Most Investment-Worthy Enterprises of the Year

2012

● In May, the internally heated ribbon vacuum dryer was designated as a Major Science and Technology Project under Zhejiang Province’s 12th Five-Year Plan

● In September, the company and the Taizhou Special Equipment Inspection and Testing Institute jointly established the Taizhou Special Equipment Welding Training and Examination Base

2013

● In March, the company joined the supplier network of China National Chemical Corporation (ChemChina)

● In July, it collaborated with Zhejiang University on an oscillatory flow reactor project

2014

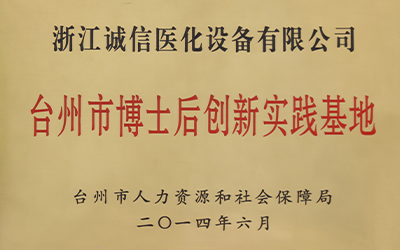
● In June, the company was designated as a Postdoctoral Innovation Practice Base

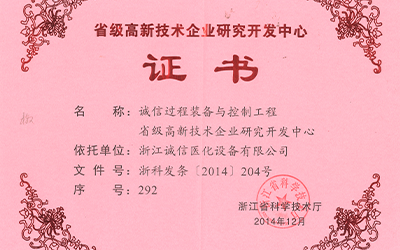
● In December, the Chengxin R&D Center for Process Equipment and Control Engineering was recognized as a Provincial High-Tech Enterprise R&D Center

2015

● In August, the company partnered with Beijing University of Chemical Technology to develop new technologies and integrated equipment systems for recovering trace organic compounds from VOC-containing waste gas and wastewater

2016

● In July, the company’s products received the Zhejiang Famous Brand designation

2017

● In April, the company relocated to its new Jiutang site, with a planned land area of 145.81 mu (approximately 8.13 hectares).

2018

● The company’s enterprise research institute was granted provincial-level status in Zhejiang, and the company received the Jiaojiang District Government Quality Award

2019

● The company was approved to establish a Zhejiang Provincial Postdoctoral Workstation

2020

● Obtained ASME certification and authorization to use the “U” Designator

● Established the Pharmaceutical Machinery Division, which commenced operations

2021

● In November, the company became a member of the China Chemical Industrial Equipment Association (CCIEA)

● In December, the company was recognized as a provincial-level specialized and innovative “Little Giant” enterprise, and its Enterprise Technology Center received provincial-level recognition

2022

● Recognized as a Zhejiang Provincial Intellectual Property Demonstration Enterprise

● Recognized as a Zhejiang Provincial Credit Management Demonstration Enterprise

● Named a “2022 Meritorious Enterprise” by Jiaojiang District

● Recognized by Jiaojiang District as a “2022 Enterprise for High-Quality Manufacturing Development”

2023

● Obtained a license for the design-by-rule of stationary pressure vessels

● Named a “2023 Meritorious Enterprise”

● The company’s laboratory obtained CNAS accreditation

2024

● Recognized as a national-level specialized and innovative “Little Giant” enterprise

● Won Second Prize in the China Industry–University–Research Collaboration Innovation Achievement Awards

● Recognized as a Zhejiang Provincial Trade Secret Protection Demonstration Site

2025

● Recognized as a Zhejiang Provincial Green and Low-Carbon Factory

● Recognized as a National High-Tech Enterprise

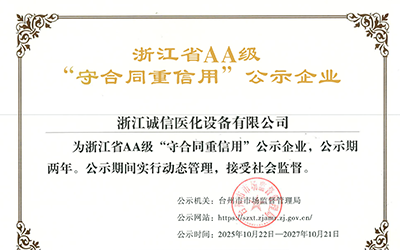
● Recognized as an AA-rated “Contract-Honoring and Creditworthy Enterprise” in Zhejiang Province

Chengxin Corporate Culture
Chengxin Spirit

Integrity, Dedication, Excellence, Innovation

Chengxin Aspirations

Sound Development, Sustainable Operations, and Progress Together with Society

Chengxin Quality Objectives

Product qualification rate upon factory release: 100%
Customer satisfaction rate:  100%

Chengxin Quality Policy

Integrity, Dedication, Excellence, Innovation
Everything We Do Is to Ensure Customer Satisfaction

Chengxin Business Philosophy

Forge Ahead, Pursue Perfection, Put Customers First, and Aim for the Highest Standards of Quality

Qualities Expected at Chengxin

Character, Ethics, Wisdom, Willpower

Market Philosophy

Professionalism Begins with Attention to Detail

Sales Philosophy

Growing Together with Our Customers

Through over 30 years of development, we have gained the trust of numerous partners.

Honors & Certifications

Over the course of its development, Chengxin has received more than 60 honors and awards and obtained nearly 20 management system certifications.

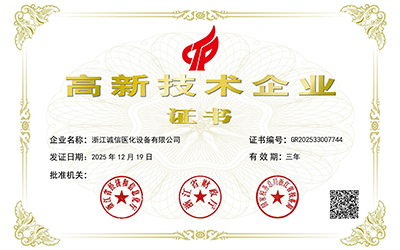
was awarded“High-tech Enterprise”certificate

2025

was awarded "National-level Specialized, Refined, Distinctive, and Novel 'Little Giant' Enterprise" certificate

2024

was awarded "Chinese Pharmaceutical Equipment Association Member Unit" certificate

2024

was awarded the "Member Unit of China Chemical Equipment Association" certificate

2021

was awarded“Zhejiang ProvinceGreen Low-Carbon Factory”Certification

2025

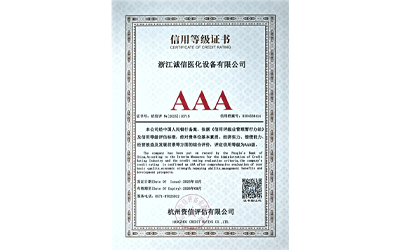
was awarded“Credit Assessment 3A Certificate”certificate

2025

was awarded Zhejiang Province "AAA Abiding by Contracts and Valuing Credit" certificate

2025

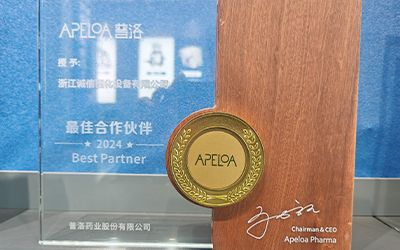
was awarded "Annual Anpel Best Partners Award" certificate

2024

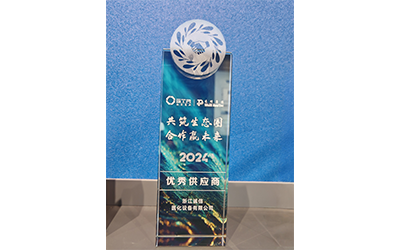
was awarded "Annual Roche-Kantar Excellent Supplier Award" certificate

2024

was awarded Zhejiang Province“Innovative SMEhonor”certificate

2024

was awarded "China Industry-University-Research Cooperation Innovation and Promotion Award" certificate

2023

was awarded Zhejiang Province“Intellectual Property Demonstration Enterprise”certificate

2022

was awarded Zhejiang Province“Credit Management Demonstration Enterprise”certificate

2022

was awarded Taizhou City“Five-star Employee Home”certificate

2022

was awarded Zhejiang University of Technology Chengxin Equipment Technology R&D Center certificate

2022

was awarded Zhejiang Province“special equipmentmember”certificate

2022

was awarded“Industrial Product Production License”certificate

2022

was awarded Zhejiang Province“Private SME High-quality Development Innovation Case”certificate

2020

was awarded Zhejiang Province“postdoctoral workstation”certificate

2019

was awarded“China Machinery Industry FederationScience and Technology Award”certificate

2018

was awarded Zhejiang Province“Provincial Enterprise Research Institute”certificate

2018

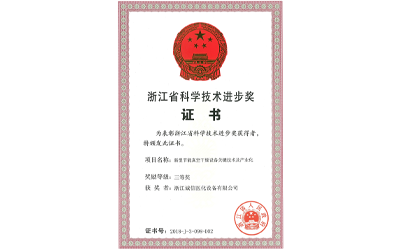
was awarded Zhejiang Province "Science and Technology Progress Third Award" certificate

2018

was awarded“Zhejiang Famous Brand Product”certificate

2016

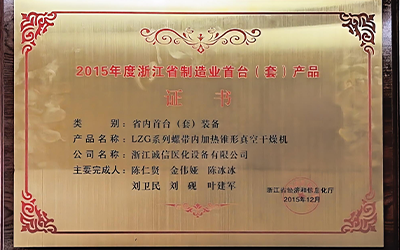
was awarded“AnnualZhejiang ProvinceFirst Manufacturing Unit Product”certificate

2015

was awarded Zhejiang Province“High-tech Enterprise R&D Center”certificate

2014

was awarded "Taizhou City Postdoctoral Innovation Practice Base" certificate

2014

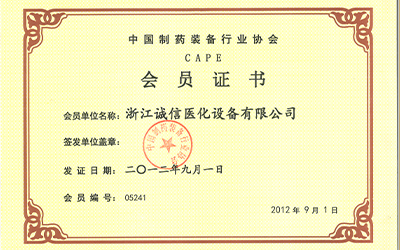
was awarded“China Pharmaceutical Equipment Industry Associationmember”certificate

2012

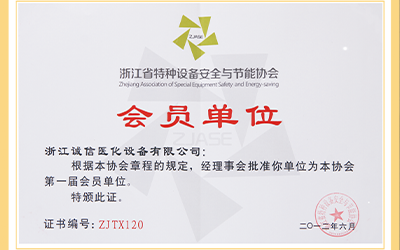
was awarded Zhejiang Province“Special Equipment Safety and Energy Conservation Association Member”certificate

2016

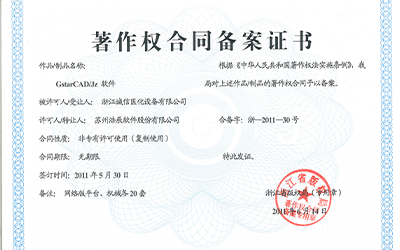
was awarded Zhejiang Province“Software Copyright”certificate

2011

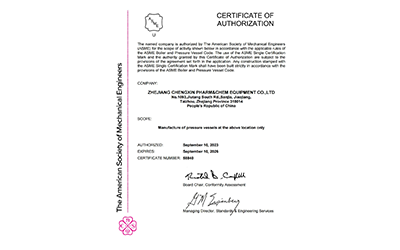
was awarded the ASME standardized "U" stamp certificate.

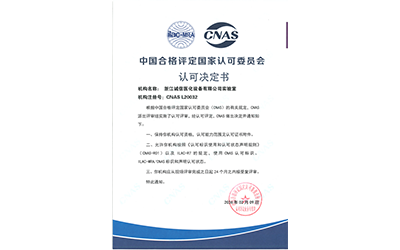
was awarded CNASlaboratoryaccreditationcertificate

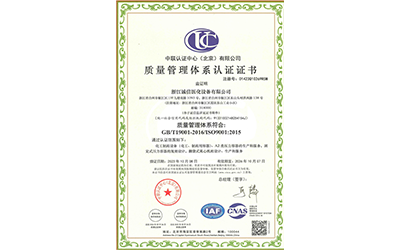
was awarded“9001Quality Management System”Certification

was awarded“Energy Management System”Certification

was awarded“Occupational Health and Safety Management System”Certification

was awarded“Intellectual Property Management System”Certification

was awarded the "Integration of Informatization and Industrialization Management System" certificate

was awarded“Environmental Management System”Certification

was awarded“Production License for Special Equipment”Certification

was awarded“Production License for Special Equipment”Certification

was awarded“Production License for Special Equipment”Certification

Honor Certificates

Certificationcertificate

The Company Has Established an Integrated Quality, Health, Safety and Environment (QHSE) Management System

The company strictly adheres to ISO 9001, ISO 14001, ISO 45001 and applicable Good Manufacturing Practice (GMP) requirements, integrating end-to-end process control across R&D, design, manufacturing, delivery and service. With quality as its foundation, safety as its top priority, environmental protection at the forefront and employee health safeguarded, the company strengthens risk prevention and control and maintains compliant operations. It continuously improves product reliability, production safety and occupational health performance. Through rigorous management standards, the company provides customers with reliable, safe and fully traceable equipment solutions for the pharmaceutical and chemical industries.

Advance a sustainable development strategy guided by the principles of green and low-carbon development, high-efficiency and circular economy, and long-term stability

Building on the ISO 50001 Energy Management System and the development of provincial-level green, low-carbon factories and water-conserving enterprises, we are deepening efforts in energy conservation, reduced consumption, clean production, and efficient resource utilization. We are focusing on the R&D of green equipment and modular and systematic construction to support the low-carbon transition of the pharmaceutical and chemical industries. We actively fulfill our social responsibilities by ensuring employee development and protecting the ecological environment, thereby achieving coordinated and sustainable development for the company, the industry, society, and the environment.