


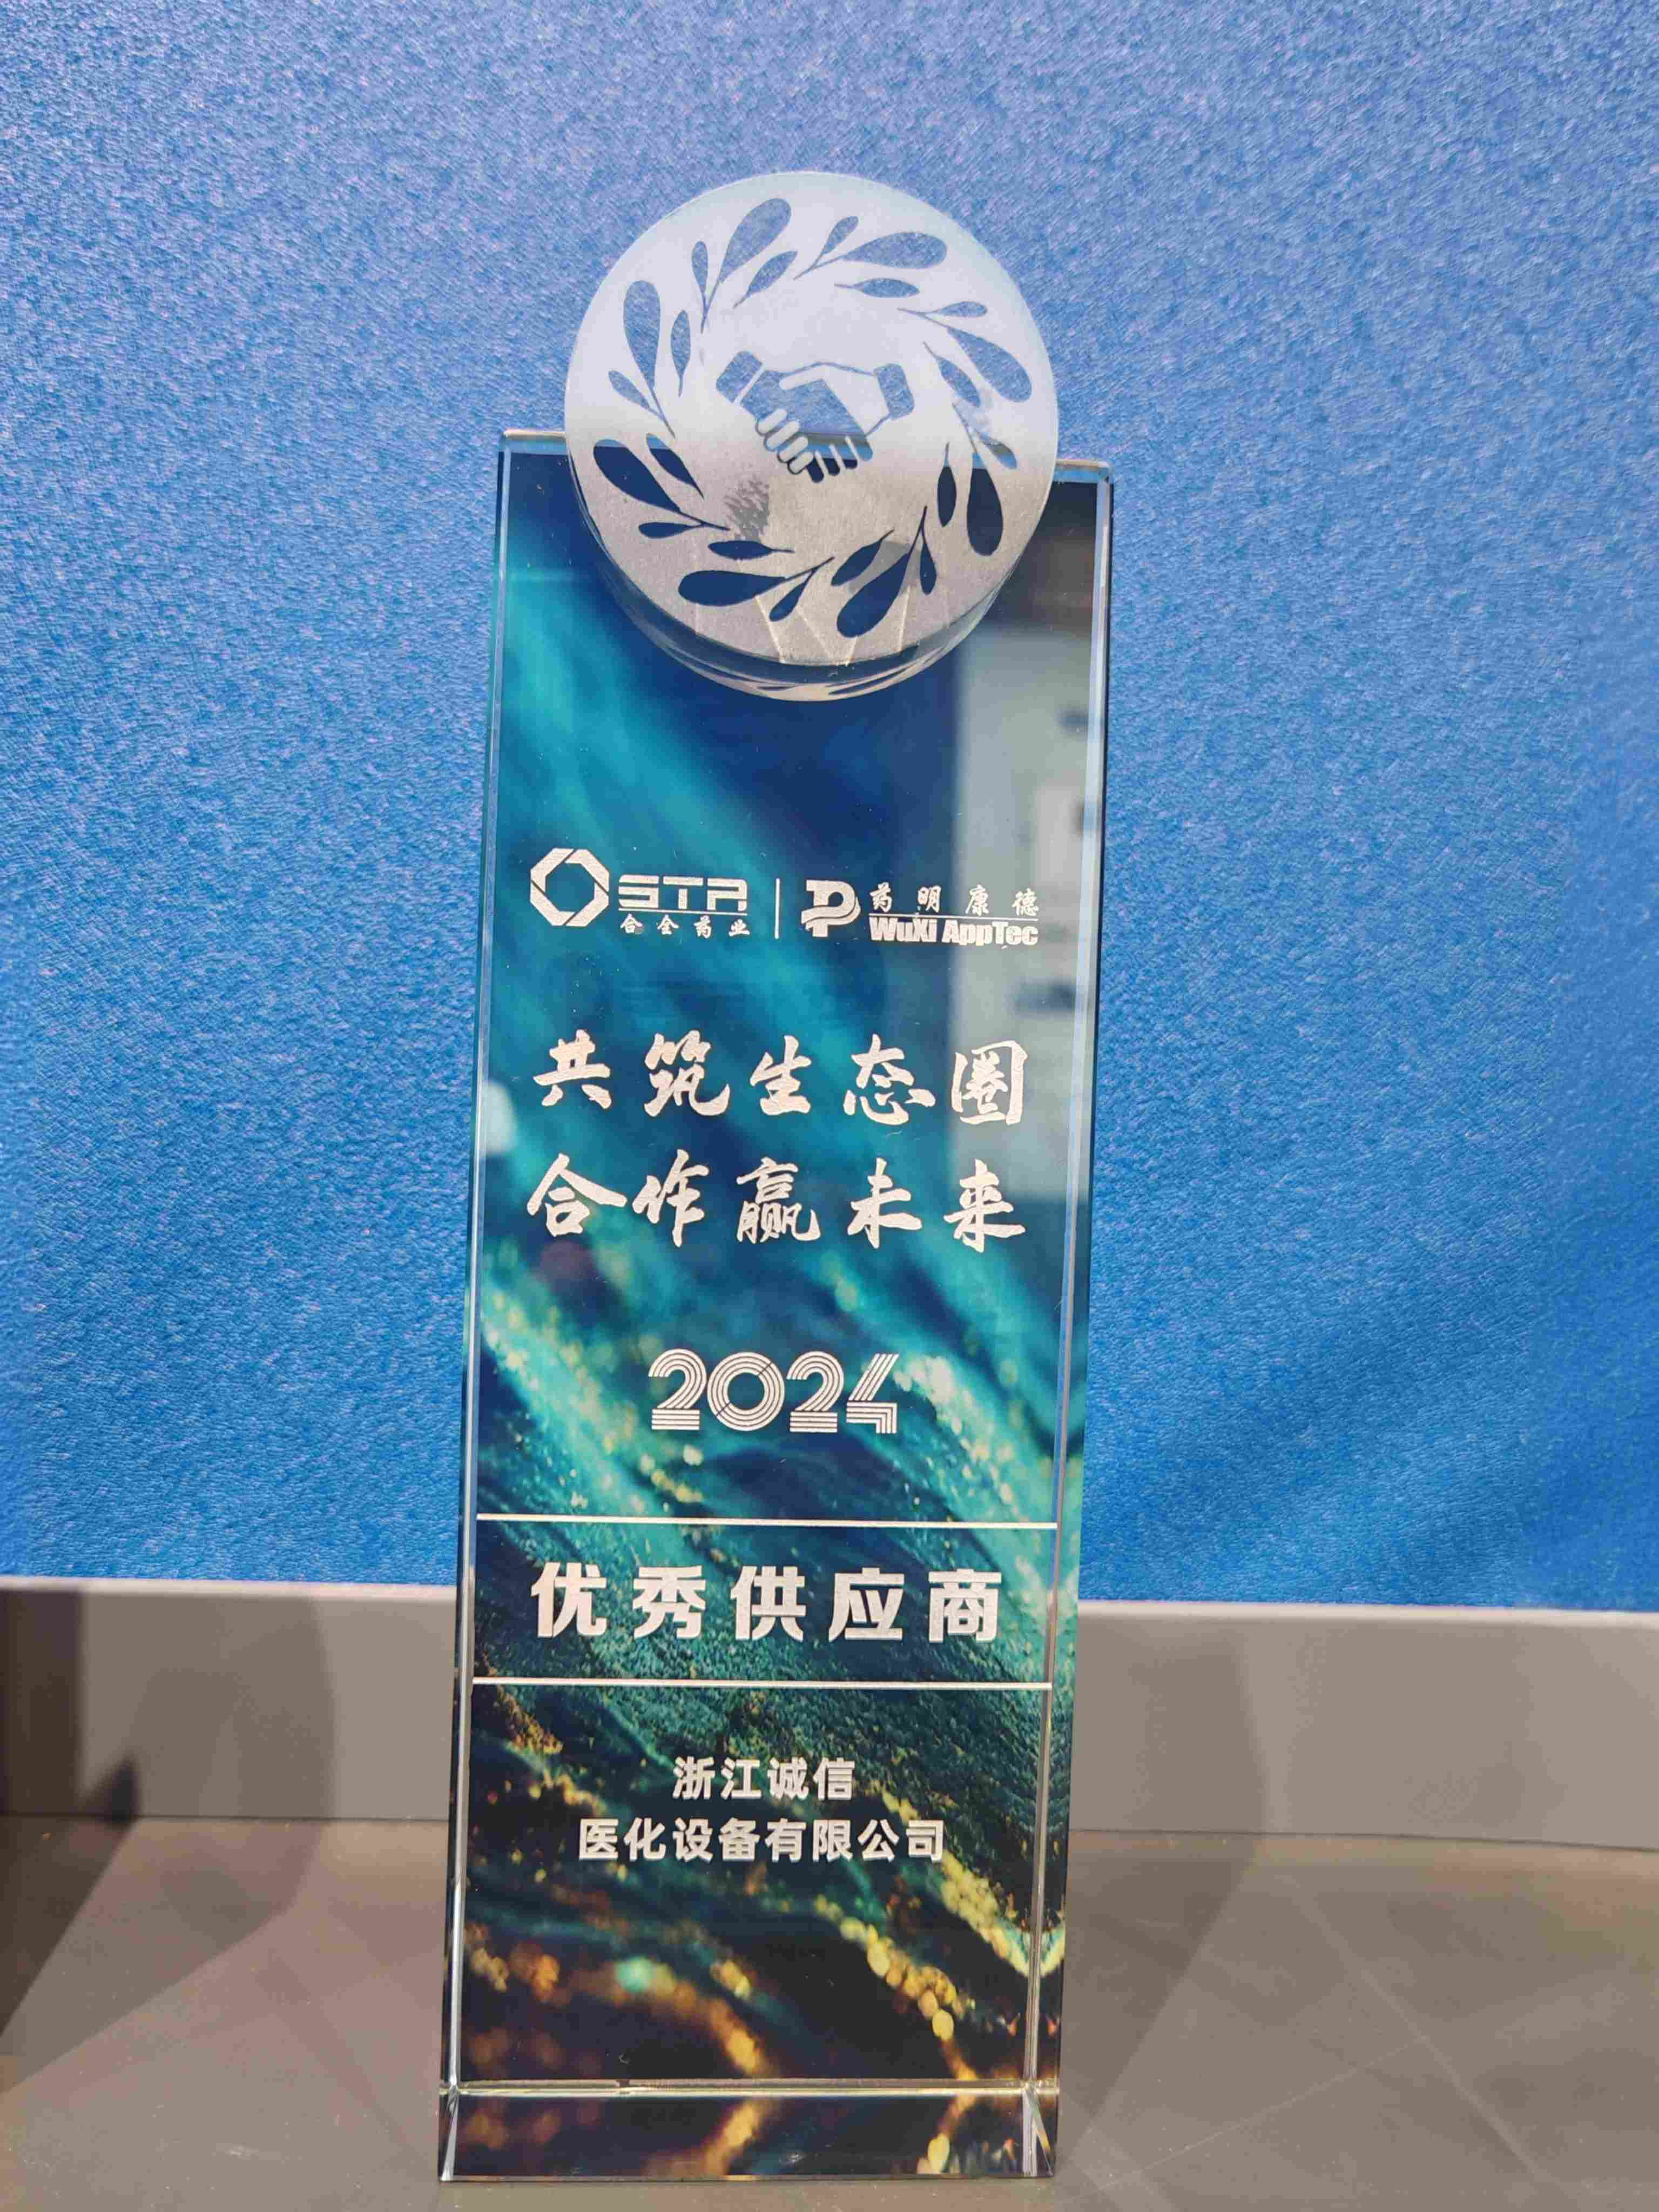
Recently, Zhejiang Chengxin Medical and Chemical Equipment Co., Ltd. was officially awarded the honorary title of "Excellent Supplier" by Wuxi Apptec Pharmaceutical for its excellent product quality and efficient service capabilities.Chen Junjia, general manager of the company, represented the team at the award ceremony and took the stage to receive the award. This award is not only a high recognition of the comprehensive strength of the company, but also marks a new stage of cooperation between the two sides in the field of pharmaceutical equipment.
As a core service provider in the pharmaceutical and health industry, Wuxi Apptec's screening criteria for suppliers cover multiple dimensions such as technological innovation, quality control, and delivery efficiency.Zhejiang Chengxin Medical and Chemical Equipment Co., Ltd. has been deeply engaged in the industry for many years, focusing on the research and development and manufacturing of pharmaceutical equipment. Its independent research and development of sterile reaction equipment, intelligent separation system and other products, because of compliance with GMP standards, stable and reliable performance, has become an important partner of Wuxi Apptec and other leading companies.This award is the inevitable result of the enterprise under the concept of "quality for survival and innovation for development".
Mr. Chen said when receiving the award:"This honor is an affirmation of the professional ability of the honest medical team, and it is a new starting point for future cooperation.We will continue to increase investment in technology, optimize supply chain services, and work with Wuxi Apptec to help the high-quality development of the pharmaceutical industry.”
The two sides will deepen cooperation in the fields of customized equipment development and digital production in the future, and jointly explore the cutting-edge direction of intelligent pharmaceutical manufacturing.
This time it was awarded the "Excellent Supplier", which not only demonstrates the leading position of Zhejiang Chengxin Medical and Chemical Equipment Co., Ltd. in the industry, but also lays a solid foundation for it to expand the domestic and foreign markets.In the future, companies will continue to uphold the business philosophy of integrity, drive industrial upgrading with technological innovation, and contribute more "Made in China" power to the global medical and health industry.