Tube reactors can be integrated with equipment such as reaction vessels and extraction tanks to form an integrated “continuous reaction–post-treatment” process line, significantly improving production efficiency and automation levels, and meeting the demands of modern factories for intelligent, large-scale production.

Automated Control

Wide Range of Applications

Sealed and Clean
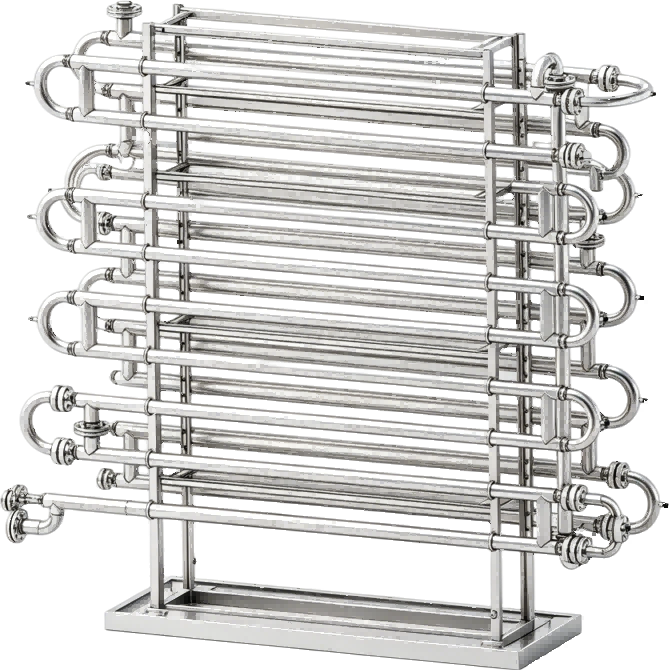

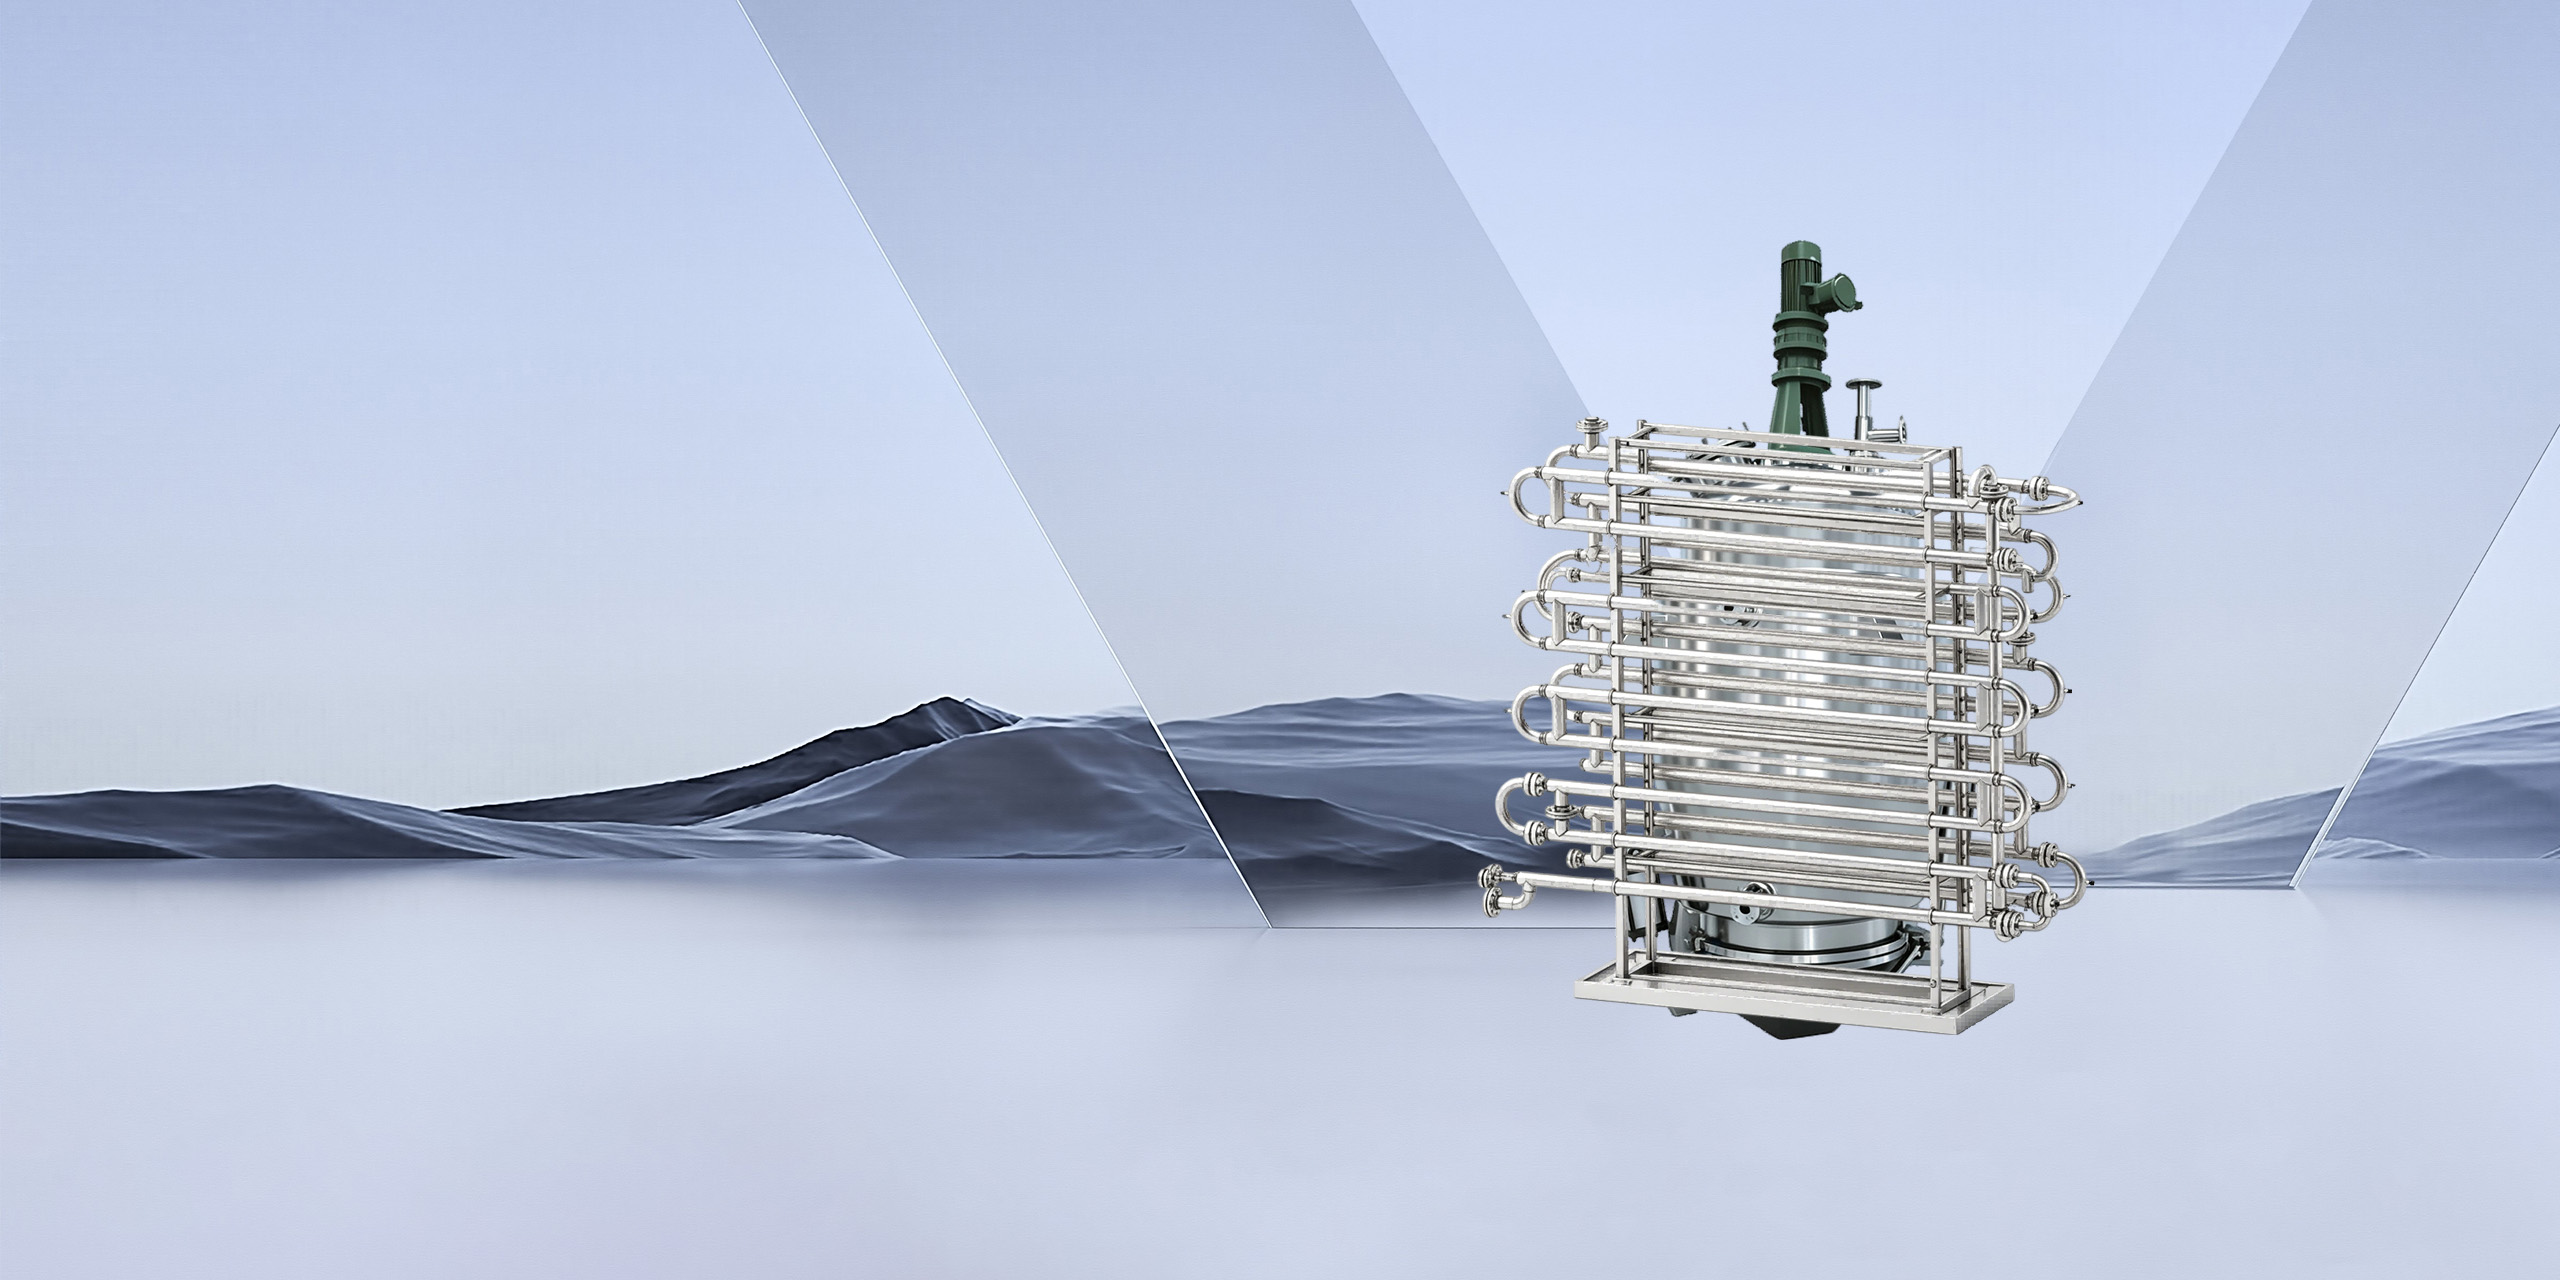
A tubular reactor is a continuous, parallel-flow reaction device designed with an optimized length-to-diameter ratio. Thanks to its efficient heat transfer, precise temperature control, and low backmixing characteristics, it enables the continuous, large-scale production of multiphase reactions such as liquid-liquid, gas-liquid, and gas-solid reactions.
The material flows continuously through the pipe in a state close to an ideal laminar flow, with uniform residence time, allowing for precise control of the reaction process and effectively preventing backmixing and side reactions.
The jacket/tube bundle design enables efficient heat exchange between the reaction medium and the heat transfer medium, allowing for precise control of the reaction temperature and making it suitable for highly exothermic or highly endothermic reactions.
The material flows turbulently through the pipe, and in combination with static mixing components, this enhances mass transfer and promotes thorough contact between reactants, significantly improving reaction efficiency and conversion rates.
Temperature and pressure measurement points, as well as sampling ports, can be installed along the pipe section to enable real-time monitoring of the reaction process and fine-tuning of parameters, ensuring product consistency across batches.
Suitable for continuous reaction processes in fields such as fine chemical synthesis, pharmaceutical intermediate preparation, environmental wastewater treatment, and food additive production; it is particularly well-suited for production scenarios characterized by fast reaction rates, significant thermal effects, and high requirements for product purity.
Pharmaceutical Industry
Fine Chemicals Industry
Food Industry
Environmental Protection Industry
Energy Industry

Composed of multiple stainless steel tubes connected in series or in parallel, it serves as the core site for continuous plug-flow reactions. It features a large heat transfer area per unit volume and high reaction efficiency.
Temperature and pressure sensors, as well as sampling valves, can be installed to monitor reaction process parameters in real time, enabling precise process control and data acquisition.
Used to introduce heating/cooling media (steam, thermal oil, or cooling water) to achieve efficient temperature control of the material inside the reaction tube, suitable for strongly exothermic or endothermic reactions.

Custom Materials

Surface Finishes

Upgraded Configurations


